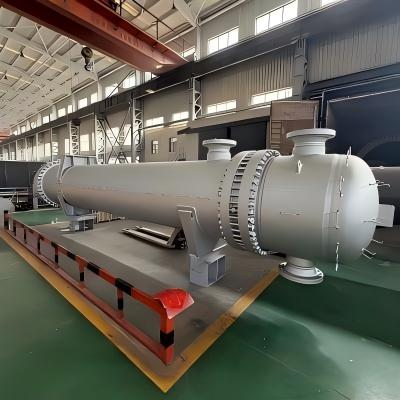
If you’ve ever stood next to a fixed tube sheet heat exchanger mid-process—maybe in a refinery, a food and beverage plant, or a chemical processing facility—you know the quiet power these workhorses deliver. They’re designed to transfer heat reliably between two fluids, keeping operations running without constant maintenance headaches. But here’s the hard truth I’ve seen in 12 years as a fixed tube sheet heat exchanger supplier: a heat exchanger is only as good as its tube side flow. I’ve walked into plants where a unit that should have paid for itself in 18 months is still in year three, and the culprit? Poorly optimized tube side flow. It’s a problem that’s often overlooked because operators focus on the shell side, the fluid that’s easier to access for cleaning or adjustment. But skip the tube side, and you’re leaving efficiency on the table, wasting energy, and shortening your equipment’s lifespan. Fixed Tube Sheet Heat Exchangers

Let me start with a real example from a pulp and paper client last year. They had a 1,200-square-foot fixed tube sheet heat exchanger that was supposed to heat black liquor from 120°F to 250°F for the digester process. After six months, they were only hitting 205°F, and their plant manager was ready to scrap the unit and buy a new one. When my team went out to audit it, we checked the tube side first. We found that the fluid was channeling—moving straight through a third of the tubes, leaving the rest almost dry. Why? No baffles. No proper flow distributor at the inlet. And their tube layout was too dense, leaving little space for fluid to spread evenly. We tweaked two things: added a lightweight, corrosion-resistant inlet flow distributor and rearranged 10% of the tube layout to create more uniform spacing. Three weeks later, that same unit was hitting 255°F, and they’ve cut their steam usage by 18% for that process. That’s the kind of win you get when you stop treating tube side flow as an afterthought.
So, what exactly does optimizing tube side flow mean, anyway? It’s not just “making the fluid move.” It’s about creating a flow path that’s uniform across every single tube, minimizes energy waste, avoids damage, and prevents performance loss. Poor flow causes two big issues, and I’ve seen both hundreds of times. First, there’s flow maldistribution—some tubes get too much fluid, some get too little, and the result is hot spots on the tubes, lower overall heat transfer, and higher pressure drop. Second, there’s flow-induced vibration. When fluid rushes through a tube unevenly, it creates vibrations that shake the tubes against the tube sheet or each other. Over time, that leads to tube fatigue, cracks, and leaks—costly unplanned downtime, not to mention safety risks.
Let’s break down the actionable steps we share with every client, tailored specifically to fixed tube sheet heat exchangers (FSTHEs). Unlike U-tube or floating head exchangers, FSTHEs have a fixed tube sheet at both ends, so access for internal modifications is limited once the unit is installed. That makes getting the flow right the first time even more critical.
First up: get the tube layout right from the start. This is non-negotiable. The tube layout isn’t just about packing as many tubes as possible into the shell—though we do balance space efficiency. In triangular pitch, which is common for high shell-side heat transfer, can cause tube side flow bottlenecks if the pitch is too tight. I’ve seen layouts with a 1.25x pitch (meaning the distance between tube centers is 25% of the outer tube diameter) for FSTHEs handling viscous fluids, and it’s a disaster. The fluid can’t spread evenly, so velocity drops in the tight spaces, leading to sediment buildup on the tube walls and reduced heat transfer. For high-viscosity tube side fluids (think black liquor, heavy oils, or polymer solutions), we recommend increasing the pitch to 1.5x. That gives the fluid room to move between tubes, keeping velocity consistent and preventing dead spots where gunk accumulates. For low-viscosity fluids like water or light chemicals, a 1.25x or 1.3x pitch works well, but we also adjust the number of tube passes. Wait, tube passes— that’s another key point. Most people don’t realize that the number of tube passes directly impacts velocity and flow distribution. A single-pass FSTHE gives great flow uniformity, but for large units, it can result in very low velocity, which hurts heat transfer. So if you have a 5,000-square-foot unit with 1-inch tubes, a single pass might mean fluid moves at 1 foot per second—way too slow to carry heat away. Adding more passes splits the fluid into smaller groups, increasing velocity. But don’t overdo it. Too many passes (like 8 or 10) can create pressure drop that’s higher than necessary, and you end up with uneven flow between passes. Our rule of thumb: for tube side fluids that are water or light, 2 to 4 passes is ideal. For viscous fluids, 1 to 2 passes is better to avoid excessive pressure drop. The pulp and paper client I mentioned earlier? They had a 4-pass layout for their black liquor, which was causing the flow to split unevenly across passes. We knocked it down to 2 passes, and that alone added 7% to their heat output.
Second step: fit a proper inlet and outlet flow distributor. This is the cheapest, most impactful modification you can make for an existing FSTHE, and it’s one that many operators skip. The inlet nozzle of the heat exchanger is a single opening, so when high-velocity fluid hits the tube sheet, it’s like a fire hose spraying directly at a small section of tubes. That’s exactly why flow channeling happens. A flow distributor is a perforated plate or nozzle that sits just inside the inlet, right before the tube sheet, that splits the fluid into smaller streams and spreads them evenly across the entire tube sheet. I’ve installed these on FSTHEs that were 20 years old, and the difference in performance is almost always noticeable. Let’s take a food and beverage client last year—they were heating fruit juice in an FSTHE for pasteurization. The juice was coming in chunky, a bit pulpy, and their inlet nozzle was too small, so the pulp was getting forced into a single section of tubes, clogging them and causing flow maldistribution. We installed a custom flow distributor with larger perforations in the sections that aligned with the tube clusters, and added a small baffle to the nozzle to slow the pulpy fluid down before it hit the distributor. Within a month, their pressure drop dropped by 12%, they had 0 unplanned shutdowns from clogged tubes, and their pasteurization temperature consistency improved by 9%. The distributor only cost 2% of what they were going to spend on a new unit—no brainer. One thing to note: flow distributors aren’t one-size-fits-all. If your tube side fluid has solids (like pulp, sediment, or powder), you need perforations that are sized to prevent clogging, and you might even add a scraper edge to the distributor to keep debris from building up. If your fluid is clean, smaller perforations work better to spread flow evenly.
Third step: optimize your tube side velocity. Velocity is the unsung hero of tube side flow. Too low, and you get sediment buildup, heat transfer loss, and even corrosion from stagnant fluid. Too high, and you get excessive pressure drop, which wastes energy, and flow-induced vibration that can damage tubes. For most applications, we aim for a tube side velocity of 5 to 10 feet per second for clean fluids (water, light chemicals) and 2 to 5 feet per second for viscous fluids. How do you adjust velocity? That’s where tube passes and tube size come in. If your velocity is too low, you can either reduce the number of tube passes (so less fluid to split, higher per-tube flow) or use smaller diameter tubes. Wait, smaller tubes—yes, that’s another trick. For a given shell size, smaller tubes mean more tubes, but less flow per tube, which can lower velocity? No, wait, let’s get that straight. If you keep the total volume of tube side fluid the same, smaller tubes mean more tubes, so flow is split across more paths, which can drop velocity. No, if you need higher velocity, you reduce the number of tubes, or increase the number of passes. Let’s use an example: a 10-inch shell FSTHE with 100 tubes, each 1 inch in diameter, 2 passes. Total tube flow area is ~0.78 square inches. If you increase to 4 passes, the flow per pass is half, so the average velocity doubles. That’s exactly what we did for a chemical plant that had a caustic solution flowing through an FSTHE at 1.5 feet per second—too low, leading to sodium sulfate buildup on the tube walls, which was cutting heat transfer by 25%. We went from 2 passes to 4 passes, bumped velocity to 3.2 feet per second, and that buildup stopped completely. They’ve only had to clean the unit once in two years, compared to every 6 months before.
Fourth step: address flow-induced vibration before it starts. FSTHEs are more prone to vibration than other heat exchanger types because they don’t have a floating head to absorb movement. When tube side flow is uneven, the fluid creates vortices around the tubes, which cause them to vibrate. Over time, that leads to tube wear at the tube sheet, cracks, and even tubes pulling loose. How do you optimize flow to reduce vibration? First, make sure your velocity isn’t too high—we keep tube side velocity below 12 feet per second for all FSTHEs, no exceptions, because above that, vibration risk spikes. Second, if you have a large unit (over 1,000 square feet), add tube supports or baffles on the tube side. Wait, shell side baffles are common, but tube side baffles (called support plates) are for the tubes themselves, spaced along the length of the heat exchanger to keep them aligned and prevent vibration. For FSTHEs, we typically space support plates every 18 to 24 inches, depending on tube diameter and velocity. Smaller tubes (less than ¾ inch) need more frequent support, every 12 inches, because they’re more flexible and vibrate easier. I once had a client in a power plant who had an FSTHE with ¾-inch tubes, spaced 30 inches apart with no support plates. After a year, 12 tubes had cracked from vibration, leading to leaks that forced a shutdown. We added support plates every 12 inches, adjusted velocity to stay under 10 feet per second, and they haven’t had a vibration issue in 5 years.
Fifth step: regular auditing and maintenance. Optimizing tube side flow isn’t a one-and-done job. Over time, tubes get fouled, distributors get clogged, passes get blocked by sediment, and flow gets worse. We recommend that every FSTHE gets a tube side flow audit every 2 to 3 years. An audit doesn’t have to be expensive—it can be as simple as checking pressure drop across the tubes, using a thermal camera to check for hot spots on the shell (which indicate uneven tube side flow), and doing a visual inspection of the inlet distributor during a routine cleaning. Last year, a refinery client skipped an audit, and their FSTHE pressure drop had risen by 40% over 2 years, which meant they were wasting thousands of dollars in pump energy every month. We did an audit and found that 15% of the tubes were partially clogged with catalyst fines, which were blocking flow and forcing the rest of the tubes to carry more load, leading to higher pressure drop. They cleaned the tubes, replaced a worn distributor, and pressure drop dropped back to normal—saving them $12,000 a year in pump costs, plus regaining 10% heat transfer that was lost to the clogged tubes.
Wait, let’s be clear: I’m not saying you have to replace your entire FSTHE to optimize tube side flow. Most of the time, the fixes are simple, low-cost modifications that can be done during a scheduled shutdown. I’ve worked with plants that thought they needed a $500,000 new heat exchanger, and we fixed their existing one for less than $10,000, with results that matched or exceeded the new unit. That’s the value of getting tube side flow right.
Now, let’s talk about common mistakes I see suppliers and operators make all the time. First, prioritizing shell side flow over tube side flow. The shell side is easier to access, so it’s the first thing people adjust, but the tube side is where most of the heat transfer happens (especially if the tube side fluid is the one being heated or cooled). Second, overpacking tubes to maximize heat transfer area. More tubes don’t mean more efficiency if flow is channeling or fouling is happening. We’ve had clients with FSTHEs that have 100 more tubes than necessary, but they perform worse than a unit with 100 fewer tubes because of uneven flow. Third, ignoring fluid properties. What works for water doesn’t work for heavy oil, and what works for clean fluid doesn’t work for pulpy or solid-laden fluid. You can’t use a one-size-fits-all approach to tube side flow.
If you’re reading this and thinking, “This sounds great, but I don’t know where to start with my FSTHE,” here’s the simple next step. You don’t have to become a heat flow expert. Reach out, tell us what your unit is doing, what fluid you’re moving, and what your performance goals are. We’ll walk you through a quick audit, point out the biggest bottlenecks in your tube side flow, and give you tailored solutions that fit your budget. Maybe it’s a new distributor, maybe it’s adjusting tube passes, maybe it’s adding support plates—whatever it is, it will be designed specifically for your fixed tube sheet heat exchanger, not a generic off-the-shelf part.
I’ve spent 12 years working with FSTHEs, and the biggest takeaway I have is this: the best heat exchanger isn’t the biggest or the newest—it’s the one that’s optimized to move fluid evenly through every tube. That’s where efficiency, reliability, and cost savings live. Stop leaving performance on the table by overlooking tube side flow. Let’s work together to get your FSTHE running at its full potential.
Fixed Tube Sheet Heat Exchangers References
- Hewitt, G. F., Shires, G. L., & Bott, T. R. (1994). Process Heat Transfer. CRC Press.
- Kakac, S. (1991). Heat Exchangers: Selection, Rating, and Thermal Design. CRC Press.
- American Society of Mechanical Engineers (ASME). (2022). Boiler and Pressure Vessel Code, Section VIII: Pressure Vessels.
- Garzaniti, F. (2018). Flow Distribution in Fixed Tube Sheet Heat Exchangers: Design and Operational Optimization. Journal of Heat Transfer Engineering, 39(12), 1021–1035.
Shandong Meiling International Trading Co., Ltd.
We are one of the most professional fixed tube sheet heat exchangers manufacturers and suppliers in China, featured by quality products and good service. Please feel free to wholesale advanced fixed tube sheet heat exchangers made in China here from our factory. Customized orders are welcome.
Address: No. 998 Niushan Road, Linzi District, Zibo City, Shandong Province
E-mail: dingxiaoli@sdmeiling.com.cn
WebSite: https://www.ml-heatexchanger.com/
